





Substation Transformer Factory Acceptance Tests: Witness Points to Agree
A transformer may be ready for dispatch while the buyer’s inspection team is still asking whether a dielectric test needed witnessing, whether a loss measurement used the correct reference temperature, or whether an unresolved deviation prevents release. These disagreements can delay shipment—or allow equipment to leave without adequate acceptance evidence. The remedy is to agree on the inspection and test plan before testing begins, not after the factory issues its report.
When working with an electrical substation transformer factory, define which activities require attendance, which cannot proceed without authorization, what constitutes a pass, and who can approve release. Routine tests must be documented for each transformer as required by the applicable standard. Temperature-rise, impulse, and other specified tests need separate decisions about applicability, witnessing, and whether existing design evidence is acceptable.
Establish the acceptance basis before booking a witness visit
The purchase specification, approved drawings, guaranteed technical particulars, and selected standards should form one consistent acceptance basis. Record the standard editions in the inspection and test plan (ITP), together with the contractual order of precedence. A report stating only “tested to IEC” is insufficient: it does not identify the applicable requirements, test conditions, or agreed deviations.
For liquid-immersed power transformers, relevant references commonly include IEC 60076-1 for general requirements, IEC 60076-2 for temperature rise, and IEC 60076-3 for insulation levels and dielectric tests. Projects using an IEEE framework may specify IEEE C57.12.00 and IEEE C57.12.90, where applicable to the transformer concerned. These frameworks should not be mixed selectively without an approved technical basis.
Test classifications also matter. Under IEC terminology, routine, type, and special tests serve different purposes; IEEE terminology and requirements should be interpreted within their own framework. Dielectric test scope depends on insulation level, winding characteristics, and the applicable standard—not simply on whether the buyer calls the transformer “distribution” or “substation” equipment.
A quality-management certificate is not a substitute for transformer acceptance evidence. Likewise, conformity markings or third-party certificates should be checked for their actual scope, issuing body, and connection to the offered design. They do not automatically prove that the serial-numbered unit passed its contractual FAT.
Distinguish attendance from permission to proceed
The most consequential ITP ambiguity is often the meaning of “witness.” Give each intervention category an explicit contractual definition:
- Hold point: work must not proceed beyond the identified stage without written authorization from the designated party.
- Witness point: the buyer receives an opportunity to attend. Proceeding without attendance is permitted only under the agreed notification and waiver rules.
- Review point: specified records are submitted for assessment; the ITP states whether approval is required before subsequent work.
- Surveillance: observation of selected activities without automatically stopping the manufacturing sequence.
For every point, identify the responsible inspector, notice period, submission requirements, and authority to waive attendance. Agree how rescheduled tests will be notified and whether remote witnessing is acceptable. A missed visit should not become an implied waiver unless the contract explicitly allows that outcome.
Remote attendance also needs practical controls: readable instrument displays, confirmed transformer identity, access to live readings, and a record linking observed activities to the report. Watching a video of the test area is not equivalent to reviewing traceable measurements.
A witness matrix that supports release decisions
The matrix below is a starting point for negotiation, not a universal mandatory test schedule. Adjust it to the transformer design, applicable standard, and consequences of failure. Specified tests remain required even when the buyer elects not to witness them.
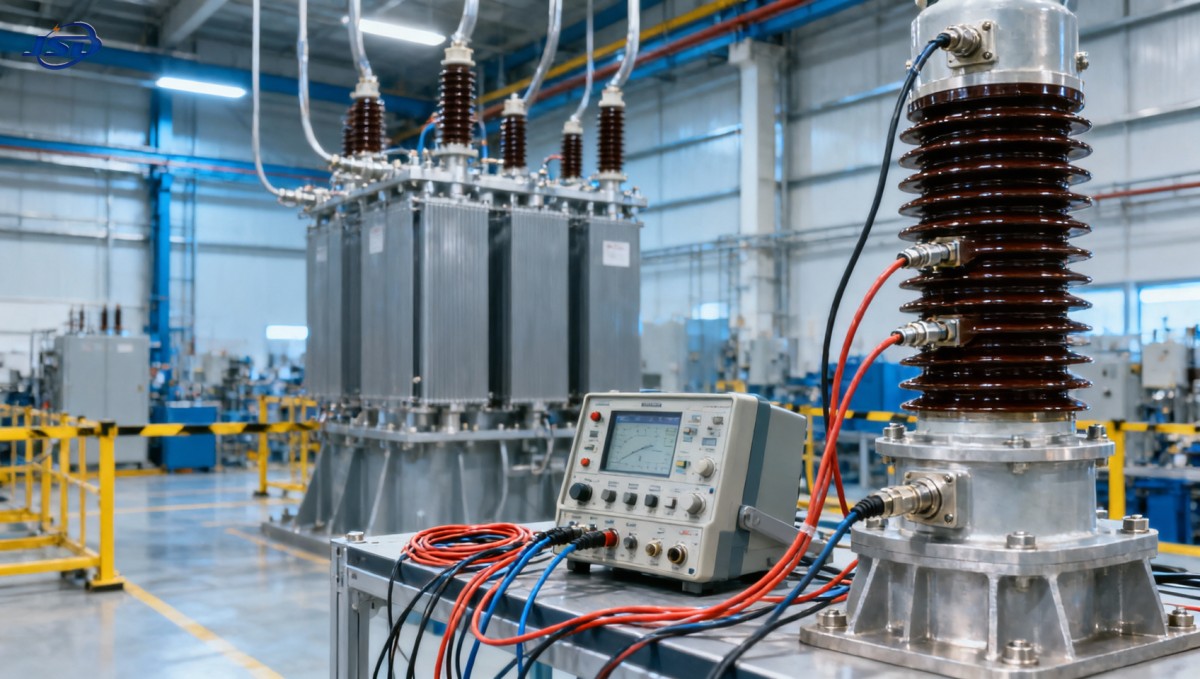
Place witnessing where observation adds information that a finished report cannot easily establish. Examples include confirming the connection arrangement, observing a dielectric test sequence, and checking how abnormal readings are handled. For lengthy thermal testing, attendance at setup, stabilization assessment, and final measurements may be more useful than requiring continuous presence.
Define the measurements—not just the test names
Ratio, resistance, and connection verification
A ratio result is meaningful only when the tested tap, terminal connections, and expected ratio are known. Agree which positions will be measured and how phase displacement and terminal markings will be verified. Do not infer the expected ratio solely from the headline voltages where winding connections affect the measurement.
Winding resistance records should identify the measured terminals, tap position, winding temperature, and stabilization method. Phase differences or unexpected tap-to-tap changes require investigation against the design and measurement conditions. Comparing readings taken at different temperatures without correction can create a false defect indication. The procedure should also address demagnetization where residual magnetism could affect subsequent measurements.
Losses and short-circuit impedance
Loss guarantees are frequent sources of acceptance disputes because the measured value and the contractual comparison value may differ. Agree the reference temperature, correction method, instrument accuracy, and treatment of measurement uncertainty before testing. Apply only the tolerances permitted by the governing standard and contract; do not introduce a general “factory allowance” afterward.
No-load measurements need the specified voltage and frequency, with supply waveform conditions controlled as required. Load-loss and impedance measurements need traceable current, temperature, and connection records. The report should show enough underlying data to reproduce corrections, rather than presenting only a final “pass” value.
An efficiency claim is not an adequate loss acceptance criterion. Efficiency depends on loading and power factor. Where energy-performance requirements apply, specify the relevant no-load and load-loss limits and assessment conditions directly.
Dielectric tests and their safety boundary
Before witnessing dielectric tests, confirm the required applied-voltage, induced-voltage, impulse, and partial-discharge activities for the particular insulation design and specification. Not every transformer requires the same combination. Establish test levels, durations, terminal treatment, sequence, and acceptance criteria from the applicable requirements.
Impulse reports, when required, should include the relevant recorded waveforms and their assessment. Partial-discharge measurements require an agreed measurement arrangement and background-noise assessment. Insulation-resistance readings may provide useful supplementary information, but they do not replace specified dielectric withstand tests.
Witnesses should remain outside controlled test boundaries. The factory’s authorized test personnel must control energization, isolation, discharge, and grounding. Agree the briefing, emergency arrangements, and communication method before testing. Buyer attendance does not transfer operational control of the high-voltage test area to the buyer.
Match thermal and liquid checks to the actual supplied design
Temperature-rise evidence must represent the agreed cooling arrangement and design. Where the contract permits an existing type-test report, confirm its relevance to the supplied transformer’s rating, losses, winding construction, cooling equipment, and insulating liquid. Acceptance of that report should occur before FAT, not when an inspector discovers that no thermal test has been scheduled.
For a configuration such as the 15kV/0.4kV Oil-Immersed Power Distribution Transformer, the order should identify the selected capacity, low-voltage rating, tap arrangement, and insulating liquid. The available range includes multiple capacities and secondary-voltage options, so a generic product description cannot establish the acceptance limits for an individual unit.
Where FR3 vegetable oil is selected, confirm that the approved thermal design, filling procedure, liquid tests, and supporting evidence apply to that liquid. Specify sampling conditions and applicable limits rather than copying mineral-oil criteria without checking their suitability.
Short-term overload capability should not be treated as permission to exceed rated-load acceptance limits during an ordinary FAT. Assessment requires an agreed loading basis, ambient conditions, previous loading, and thermal limits. Oil temperature alone does not establish winding hot-spot temperature or insulation-aging acceptability.
Keep deviations visible until they are formally closed
An abnormal result should trigger a controlled investigation, not repeated testing until a passing number appears. Preserve the original reading and record the suspected cause, corrective action, and authorization for retesting. Distinguish a measurement problem from a transformer defect: both require evidence, but their corrective actions and implications differ.
- Record the deviation: identify the serial number, test, requirement, observed result, and affected documents.
- Assess its consequences: determine whether insulation integrity, guaranteed losses, thermal performance, accessories, or other results may be affected.
- Approve corrective action: identify any repair, adjustment, replacement, or procedure change and the required inspection stages.
- Define retest scope: repeat the failed activity and any other tests made necessary by the intervention, standard, or contract.
- Close through authorized acceptance: retain the original and revised evidence, with a signed disposition.
A repair involving active parts or insulation can invalidate more evidence than an external accessory replacement. Retest scope should therefore reflect what changed, not merely reproduce the last failed measurement. Acceptance “as is” requires the buyer’s designated engineering authority where contractual performance or safety requirements are affected.
Make shipment release a separate authorization
Passing the final witnessed test does not automatically authorize dispatch. The release hold should cover the complete serial-numbered report, approved deviations, calibration references, nameplate verification, accessory records, and the agreed shipment condition. Where liquid sampling or leak checks are required after final assembly, those records must also be available before release.
The dispatch inspection should verify transport restraints, bushings and accessories, preservation measures, liquid condition or level as applicable, and any shock-monitoring arrangements specified in the contract. FAT establishes factory acceptance under defined conditions; it does not demonstrate that transport caused no damage or that site connections are correct.
The signed release should state precisely what is authorized: acceptance of the FAT evidence, permission to ship, and any remaining obligations. Site inspection and commissioning remain separate activities. An unresolved safety-critical or contractual deviation should not be hidden in a punch list simply to maintain the dispatch date.

Get a Quote
Regardless of whether you require general advice or specific support, we are happy to help you.
Send Us Your Inquiry Today

Jinshida Electric remains committed to contributing to global energy development through professional manufacturing and superior service.