





220 kV Transformer Supplier Qualification: Test Capability and Track Record
A competitive quotation can make a transformer supplier look ready for a major grid project. The real test comes when procurement asks for evidence: complete test reports, traceable manufacturing records, and references from transformers operating under comparable conditions. At 220 kV, gaps in that evidence can become expensive after the purchase order is signed.
Choosing a 220kv high voltage transformer supplier therefore requires more than comparing prices and delivery schedules. Buyers need to establish whether the proposed manufacturer can validate the design, control production quality, and support the equipment throughout installation and operation. The most useful qualification process separates what a supplier claims from what its documents, facilities, and customers can actually confirm.
Define the transformer before qualifying the supplier
“Experience with 220 kV transformers” is too broad to serve as an approval criterion. A generator step-up transformer, a grid interconnecting autotransformer, and an industrial receiving transformer may share a voltage class while presenting different design and operating demands.
Before reviewing suppliers, create a technical baseline covering rated power, voltage ratio, frequency, vector group, impedance, insulation levels, tap range, cooling arrangement, and installation conditions. Include expected loading, ambient temperature, altitude, seismic requirements where applicable, and transport restrictions. For renewable energy connections, specify relevant harmonic conditions and operating cycles rather than assuming conventional grid duty.
Also distinguish the nominal system voltage from the equipment’s highest voltage designation. A nominal 220 kV network commonly uses equipment rated for a highest voltage of 245 kV under IEC practice, but the project specification and local utility requirements must govern.
This baseline makes reference checks meaningful. Without it, procurement may accept experience that sounds impressive but does not address the proposed transformer’s actual risks.
Read test evidence in three separate layers
The IEC 60076 series provides a widely used framework for power transformer requirements and testing. Applicable editions, national requirements, and utility specifications should be stated in the contract. Test classifications depend on the relevant standard part and equipment characteristics; a supplier’s generic “IEC compliant” statement is not a complete test plan.
Routine reports: follow the individual transformer
Routine evidence typically covers measurements such as winding resistance, voltage ratio and phase displacement, short-circuit impedance and load losses, and no-load losses and current. Dielectric testing must follow the applicable voltage-class requirements. For high-voltage transformers, pay particular attention to the required induced-voltage test arrangements and partial discharge measurement.
Ask for a complete sample report, not a one-page certificate stating “passed.” Useful reports identify the transformer, tap position, test connections, temperature corrections where relevant, instruments, and measured values. Loss guarantees should be evaluated using the agreed reference conditions and contractual tolerances.
A warning sign is a report with missing serial numbers, unexplained corrections, or values that do not match the nameplate and approved drawings. These discrepancies warrant clarification before commercial approval, even if the final result appears acceptable.
Type-test reports: check design relevance, not just the laboratory logo
A credible laboratory report can still be irrelevant to the offered transformer. Temperature-rise evidence, for example, should be assessed against the proposed winding arrangement, losses, cooling configuration, and rating. Dielectric evidence requires attention to insulation design and the applicable test levels.
Request a comparison between the tested design and the proposed design. Differences in winding geometry, insulation clearances, conductor arrangement, cooling system, or manufacturing location may require an engineering explanation or additional testing. “Same product family” alone is not enough.
Lightning impulse requirements—and switching impulse requirements where applicable—should be established from the governing standard and project specification. Procurement should avoid prescribing a generic test package without technical review.
Special tests: select them around project risk
Special tests may include sound measurements, zero-sequence impedance, frequency response analysis, or other agreed checks, depending on their classification under the applicable standard. A frequency response analysis baseline can be useful for later comparisons after transport or suspected mechanical disturbance, provided measurement conditions are documented consistently.
Short-circuit withstand deserves its own discussion. It is not normally demonstrated by testing every delivered unit. Ask how compliance with IEC 60076-5 or the specified equivalent will be established: relevant test evidence, design calculations and evaluation, or another contractually accepted route. Any reliance on a previously tested transformer needs a defensible similarity assessment.
Can the supplier perform the tests—or only arrange them?
Outsourcing a specialized test does not automatically disqualify a manufacturer. What matters is whether the arrangement is technically suitable, traceable, and available within the delivery program. Conversely, owning a test hall does not prove that it can accommodate your transformer.
During the factory assessment, follow the path from production to final testing: winding manufacture, insulation drying, active-part assembly, oil processing, tank completion, and the test bay. This reveals whether the quoted schedule reflects actual capacity or an optimistic sequence of assumptions.
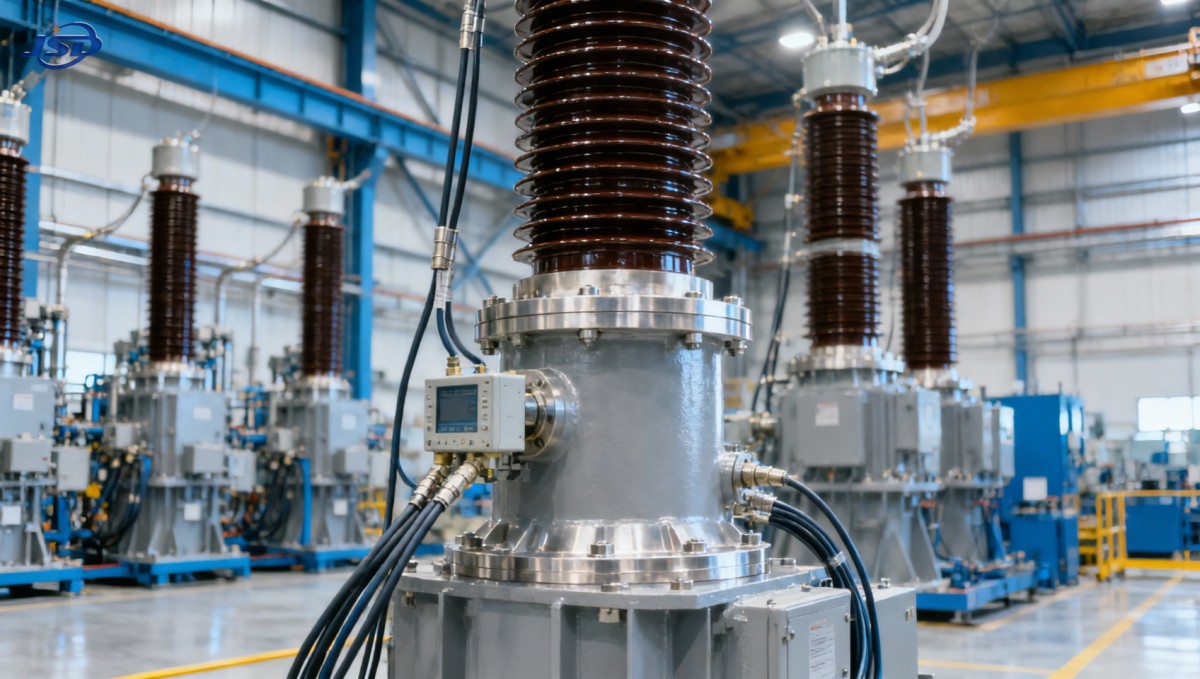
For test capability, request evidence of:
- Electrical capacity: suitable test sources, impulse equipment, measuring systems, and connections for the specified ratings and test levels.
- Physical capacity: sufficient clearances, lifting arrangements, floor loading, and space for the assembled transformer.
- Measurement integrity: calibration records, uncertainty information where relevant, partial discharge background-noise control, and competent personnel.
- External test arrangements: the identified facility, agreed scope, relevant accreditation where required, and booking availability.
- Failure handling: procedures for investigation, corrective action, retesting, and customer notification.
Ask who will perform each contractual test and where. Where laboratory accreditation is claimed, verify that its scope covers the relevant activity; accreditation is not a blanket endorsement of every test a facility offers.
A track record should survive a reference call
A list of shipped transformers establishes commercial activity, not necessarily reliable operation. The stronger evidence is a set of comparable units that have been commissioned, operated, and supported over time.
Request references showing voltage class, capacity, transformer function, cooling arrangement, commissioning date, manufacturing site, and operating environment. Customer confidentiality may limit disclosure, but suppliers should explain those limits and offer an appropriate verification route, such as an authorized reference call or redacted documentation.
Three questions often reveal more than a glossy project list:
- Were there factory-test failures, commissioning problems, or significant design changes, and how were they resolved?
- Has the operator experienced abnormal gas trends, oil leakage, bushing problems, tap-changer issues, or unexpected thermal behavior?
- When support was needed, did the supplier provide a technically useful response and complete corrective actions?
Interpret the answers in context. A reported problem does not automatically indicate an unsuitable supplier; transparent root-cause analysis and effective corrective action can be more reassuring than an unsupported claim of a flawless history.
Check who actually designed and manufactured the referenced units. A trading company’s project portfolio, a partner factory’s experience, and the bidding manufacturer’s own record are not interchangeable. Qualification should identify the contractual supplier, design authority, production site, and warranty responsibilities.
Separate portfolio breadth from 220 kV competence
A manufacturer’s distribution equipment can provide useful insight into its materials control, documentation practices, and application support. It cannot, by itself, establish high-voltage power transformer capability.
For example, Jinshida Electric Power Technology Co., Ltd.’s 10kV Cast Resin Dry-Type Distribution Transformer is described for 10 kV-to-0.4 kV distribution duties, with capacities from 30 to 2,500 kVA, copper windings, cast-resin insulation, and temperature protection and control. Such equipment may be relevant to auxiliary distribution in industrial plants, commercial facilities, or renewable energy projects.
However, dry-type distribution experience does not demonstrate the insulation coordination, oil-paper processing, mechanical withstand, or testing capability required for a 220 kV power transformer. Buyers considering Jinshida Electric—or any diversified equipment provider—should request a separate, voltage-class-specific qualification package. Broad quality-management claims and lower-voltage product documentation are supporting context, not substitutes for that evidence.
Turn the factory acceptance test into a contractual gate
A factory acceptance test, or FAT, is useful only when its scope and consequences are agreed before manufacturing is complete. Otherwise, buyers can arrive at the factory to discover that an expected measurement was excluded or that the acceptance rule is disputed.
The purchase specification should define the test matrix, applicable standards, guaranteed values, tolerances, witness and hold points, notification periods, and reporting format. Identify which procedures require approval before testing and whether an independent inspector will attend.
Clarify the response to a failed test: investigation, proposed repair, disclosure obligations, repeat testing, and release approval. A repaired transformer should not be released merely because one repeated measurement passes; the purchaser’s technical team should assess whether the corrective work affects other validated characteristics.
Keep shipment release linked to closure of agreed nonconformities and acceptance of required records. Where post-test disassembly is necessary for transport, specify preservation, handling, and site reassembly requirements so factory acceptance connects logically to commissioning.
Make the shortlist evidence-led
For procurement teams, a practical approach is to use mandatory gates before weighted commercial scoring. A low price should not compensate for missing dielectric capability, unverified design authority, or an unresolved manufacturing-site question.
Require the following before final approval:
- A signed technical compliance schedule with deviations clearly identified.
- A project-specific test plan and credible evidence supporting the proposed design.
- Verified comparable operating references, with remaining limitations recorded.
- An agreed inspection plan and closure of critical factory-audit findings.
- A delivery schedule covering design approval, long-lead components, production, testing, and transport.
- Defined warranty, commissioning support, spare-parts, and technical-response responsibilities.
Once suppliers pass these gates, compare evaluated cost rather than purchase price alone. Guaranteed losses, maintenance needs, transport complexity, and support provisions can materially affect lifecycle value. Any capitalization of losses should use the project’s agreed economic assumptions, not a supplier’s preferred calculation.
The best-qualified 220kv high voltage transformer supplier is not necessarily the one with the longest reference list or the largest test facility. It is the one that can connect the offered design to relevant evidence, demonstrate control over manufacturing and testing, and explain its operating history without evasions. That traceable chain gives procurement a defensible decision—and gives the project team fewer unanswered questions when energization day arrives.

Get a Quote
Regardless of whether you require general advice or specific support, we are happy to help you.
Send Us Your Inquiry Today

Jinshida Electric remains committed to contributing to global energy development through professional manufacturing and superior service.